Introduction: A Practical Lens on Factory Choices
Quality in batteries is not an accident; it is a sequence of controlled steps, measured in minutes and milliohms. Energy storage battery companies live or die by this simple truth. In May 2023, during an audit at an energy storage lithium battery factory in Xiamen, I watched a line supervisor switch the tab-welding camera from generic contrast to edge-detection mode. One small change. Yet the weld rework rate fell from 4.6% to 1.9% in three shifts, and module impedance variance tightened by 0.3 mΩ. With respect, that is not a miracle; that is process discipline. We measured OEE improvement from 66% to 74% within two weeks—helped by better SoC calibration and a cleaner DC bus on the formation racks.
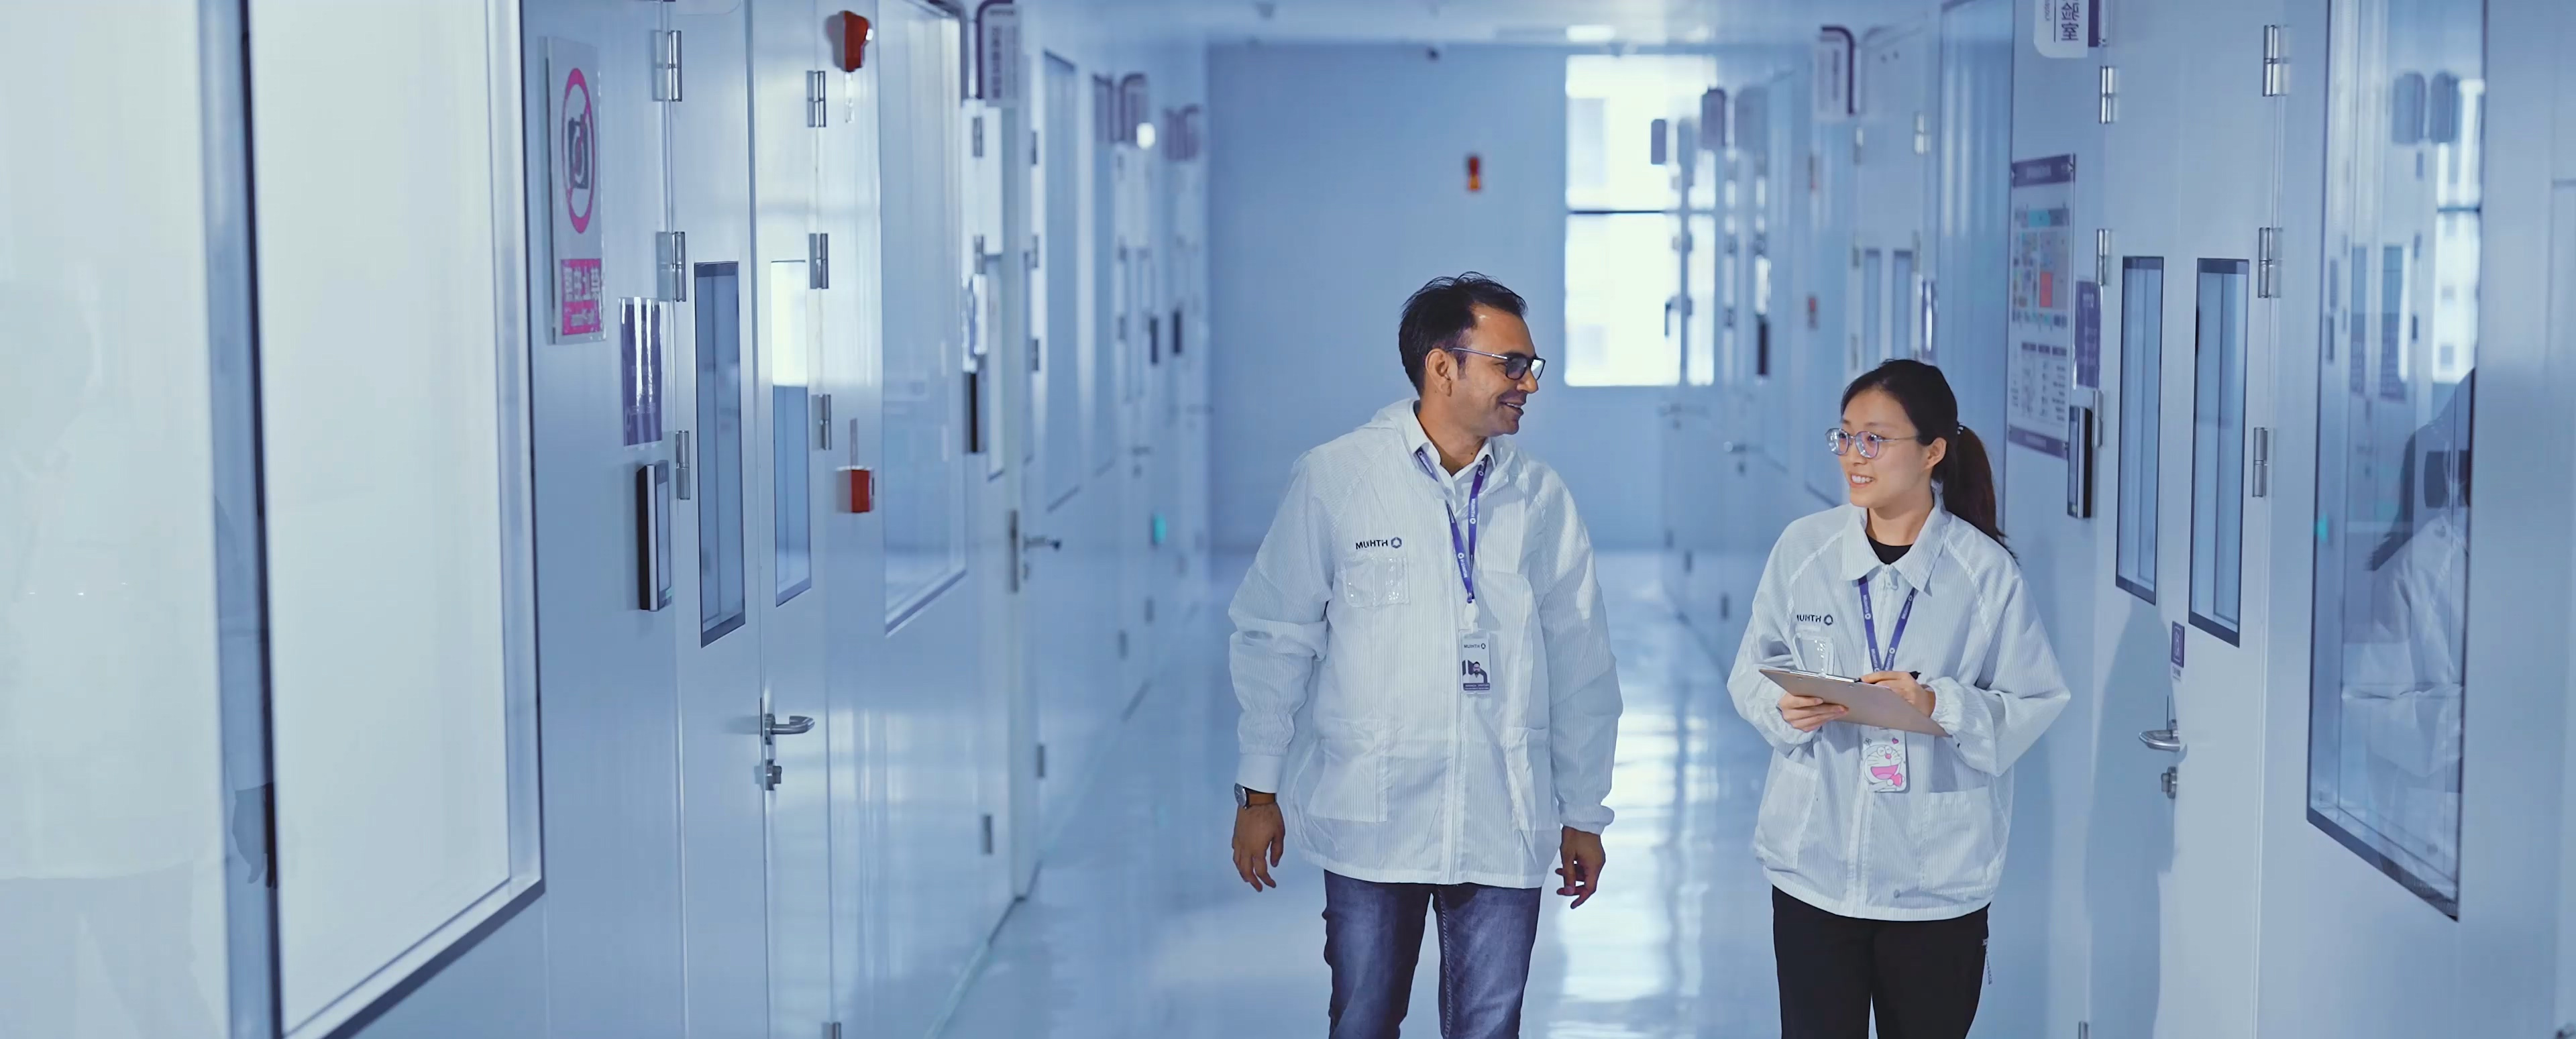
I have spent over 15 years helping procurement heads and EPC teams choose the right partner plants, from Suzhou to Ras Al-Khair. I learned to trust boring metrics: dew point at the dry room (-45°C or better), BMS calibration drift under 0.5%, and power converter harmonics below 3%. When those are right, the big promises start to come true. So let me compare what sounds smart with what actually works—so you can buy with clarity.
Comparative Insight: What Looks Good vs. What Works
Where do common fixes fail?
Many buyers ask for more robots and more dashboards. I understand; automation sounds safe. But I keep seeing the same blind spots inside a busy energy storage lithium battery factory: no enforced rest window after cell formation (less than 24 hours leads to noisy OCV readings), loose traceability between electrode batch and module ID, and BMS shunt tolerances drifting 1–2% after thermal cycling. These look small. They are not. A 1.5 mm tab misalignment on a 280 Ah LFP prismatic cell adds about 0.4 mΩ. That costs roughly 0.8% energy per cycle at the pack level—quiet leakage of value. When I saw a crate stored at 55% RH near the sealing area—yes, next to the door—I knew we would find early corrosion on the busbar plating before FAT. I said it aloud, and yes, I winced when I saw it.
Another place where “traditional fixes” disappoint is the power path. Teams upgrade the EMS and add a shiny dashboard, but they leave the PCS filters and grounding scheme unchanged. Result: harmonics creep in, SoH estimation gets jumpy, and crews chase the wrong symptom. Let me be frank—this part trips teams more than they admit. Fix the power conversion system first, then let the edge computing nodes clean the data. Also, enforce ion chromatography checks on the separator lots weekly, not monthly. It is dull work, but the cycle life curve will thank you.
Forward Look: Principles That Outperform Hype
What’s Next
When I compare two lines—one “modernized,” one truly modern—the difference sits in a few technical principles. First, inline EIS on the formation racks beats post-process sampling. It cuts false positives during cell grading by half, in my experience across three plants between 2022 and 2024. Second, machine-vision that measures weld nugget diameter, not just presence, reduces latent defects in busbar joints. Third, a dry room that holds a stable -50°C dew point (not average, but P95) gives you fewer lithium plating events under fast charge at 1C. These are not slogans; they are the spine that holds yield steady. I saw a line in Xiamen shift to closed-loop calendaring pressure control; thickness variance dropped from 5.2 μm to 2.1 μm in one week—quiet change, big outcome.
Looking ahead, the better energy storage lithium battery factory will push compute to the edge. Put the anomaly detection next to the laser tab welder, not only in the MES. Use a local model to flag spatter morphology outside control limits in under 200 ms. Then feed only the exceptions upstream to the EMS. This protects the pack assembly pace, keeps the DC bus clean, and avoids drowning staff in alerts. Module-level liquid cooling manifolds with verified flow balance (±3%) will become standard on high-density racks. And the smarter plants will publish a weekly control-plan digest to buyers—small, precise, and accountable. I prefer that approach, because it respects your time and your risk tolerance—odd, but fixable when someone takes ownership.
If you are choosing between suppliers, set your evaluation on three practical metrics. One: traceability granularity from slurry lot to pack serial, with query time under 30 seconds. Two: verified process capability on three steps—calendaring, laser tab welding, and formation SoC cut-off—each at Cpk ≥ 1.33 over the last 90 days. Three: power conversion cleanliness, measured as THD under 3% at full load and ground impedance documented below 1 Ω. With these in hand, you cut rework, speed FAT, and reduce surprise warranty calls by real numbers, not wishful thinking. This is how I advise procurement managers, politely but firmly. And if a plant already meets that bar, I take a breath and say, let us build on that foundation with care. HiTHIUM